

Complete Tool Move-In for a New Semiconductor Fab: Sustained Programme Execution at Scale
Categories
Introduction
A single tool move requires planning and discipline. A programme of more than 100 tool moves, compressed into a tight window against a go-live date, requires something more — the operational capacity to sustain that standard across every move, in sequence, without the performance degrading as the volume builds.
When a leading semiconductor manufacturer opened a new fabrication facility, B H S was commissioned to execute the full tool move-in programme: tools and their bespoke anti-vibration pedestals, moved into position across a partially constructed site over a period of weeks. The programme ran alongside active construction, coordinated against the fab’s placement schedule, and sustained the same handling standard from the first tool to the last.
This case study is not about a single move. It is about what it takes to run a sustained programme at this scale without losing control.
The Customer’s Challenge
A complete tool move-in for a new fab is not a series of identical jobs. The site conditions change as construction progresses. The placement sequence creates dependencies. The go-live date does not move. And the standard applied to the hundredth tool has to match the standard applied to the first.
- Scale compounds every operational challenge. At low volume, a planning gap or a sequencing error is recoverable. At more than 100 tools, a missed step early in the sequence has downstream consequences that take days to resolve.
- The site changes every day. Construction zones hand over to cleanroom zones progressively. The move-in programme has to absorb those changes without disrupting the placement sequence the fab requires.
- Tools and pedestals are paired and sequenced. Each tool requires a bespoke anti-vibration pedestal. The pedestal goes in first. The tool follows. Across more than 100 pairs, managed across multiple zones and multiple weeks, that pairing discipline has to hold without exception.
- The go-live date is the customer's public commitment. A semiconductor fab opening is not an internal milestone. It is a commitment made to customers, investors, and the market. Every day the move-in slips is a day closer to missing that commitment.
- Sustained performance over weeks, not hours. A team can hold its highest standard for a single move. Holding that standard across weeks of continuous programme execution, in a physically demanding environment, requires planning, supervision, team management, and the ability to adjust without losing momentum.
The B H S Solution
Programme Planning Before the First Move
Before a single tool was touched, B H S developed the full programme plan with the fab’s industrial engineers. The placement schedule was mapped against the construction programme and the physical conditions of each zone. The bespoke lifting platforms required for the site were designed and fabricated by B H S in advance.
Access protocols for working across both construction and cleanroom zones were established before work started.
Warehouse Staging and Sequenced Release
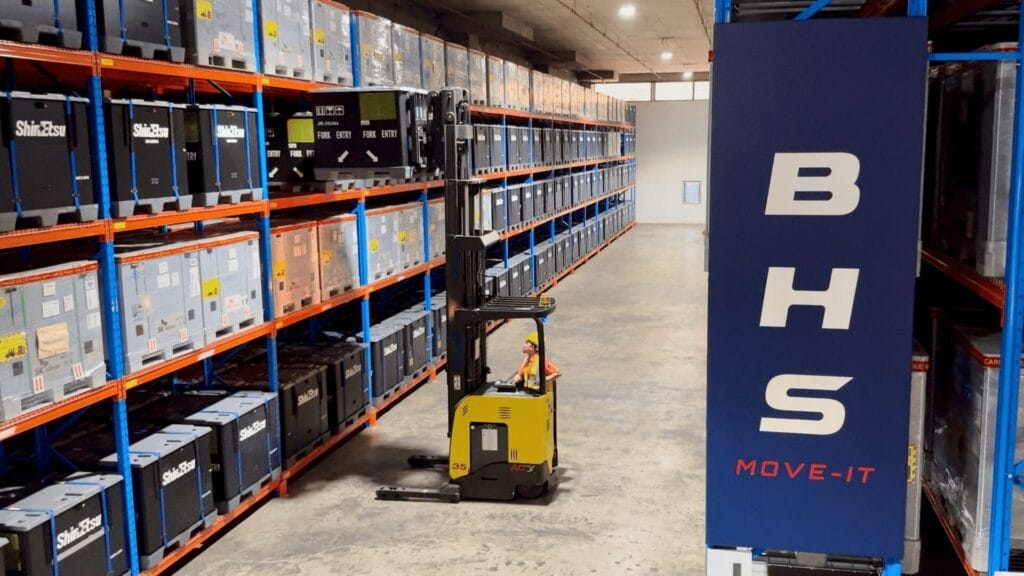
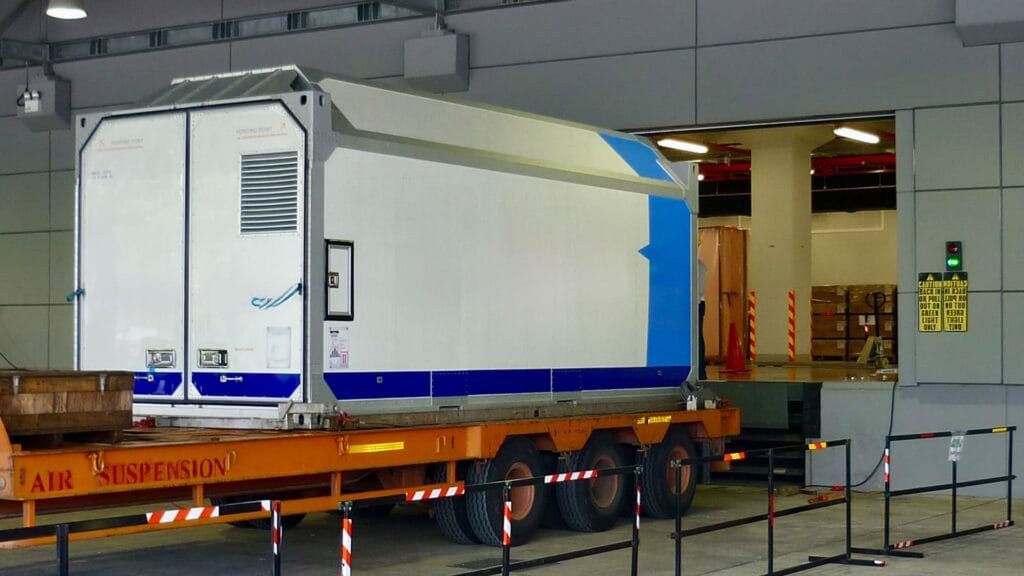
The tools arrived from manufacturers across multiple countries throughout the programme period. Arrival order was determined by international freight — not by the placement sequence the fab required. B H S received each tool at its warehouse as it arrived, held it under controlled conditions, and released it to site in the sequence the fab’s industrial engineers specified.
At no point was a tool released to site before the placement sequence required it. The staging programme absorbed the unpredictability of international freight arrivals and construction progress, so that neither passed through to the fab’s go-live schedule.
Pedestal Installation Using Jacking and Skidding
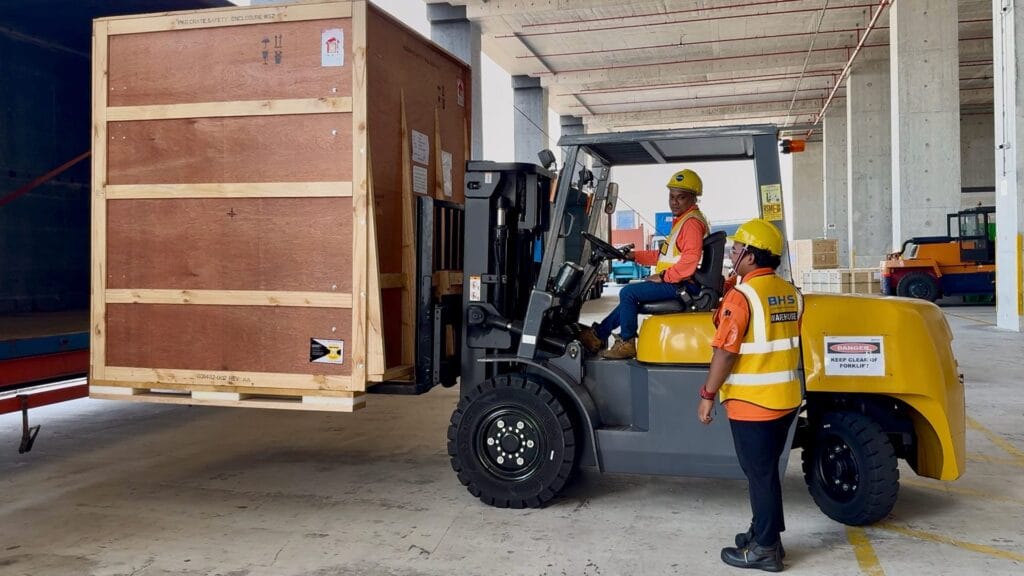
Each anti-vibration pedestal was positioned according to the fab’s placement drawings. Where the raised cleanroom floor configuration and tight tolerances required controlled incremental movement rather than a single lift, B H S used jacking and skidding techniques — moving the pedestal into its precise position in small, controlled increments. The facility team confirmed alignment before the corresponding tool followed.
Tool Rigging and Cleanroom Installation
With each pedestal confirmed in position, B H S rigged the corresponding tool into the cleanroom and positioned it on the pedestal. Cleanroom protocols were maintained throughout the finished zones. The move-in proceeded as a managed sequence, not a series of parallel independent lifts. Progress was tracked against the placement schedule daily.
Sustained Programme Management
Across a move-in programme of this scale, the challenge is not the first day. It is maintaining the same standard on the fortieth day as on the first. B H S managed the programme through daily coordination between the site team, the warehouse staging operation, and the fab’s industrial engineers. Sequencing decisions, access changes, and equipment requirements were managed in real time.
Results and Impact
- Full programme completed against the go-live date. All tools and their bespoke pedestals were installed in the sequence the fab required, within the compressed move-in window, allowing the fab to proceed to commissioning and open on schedule.
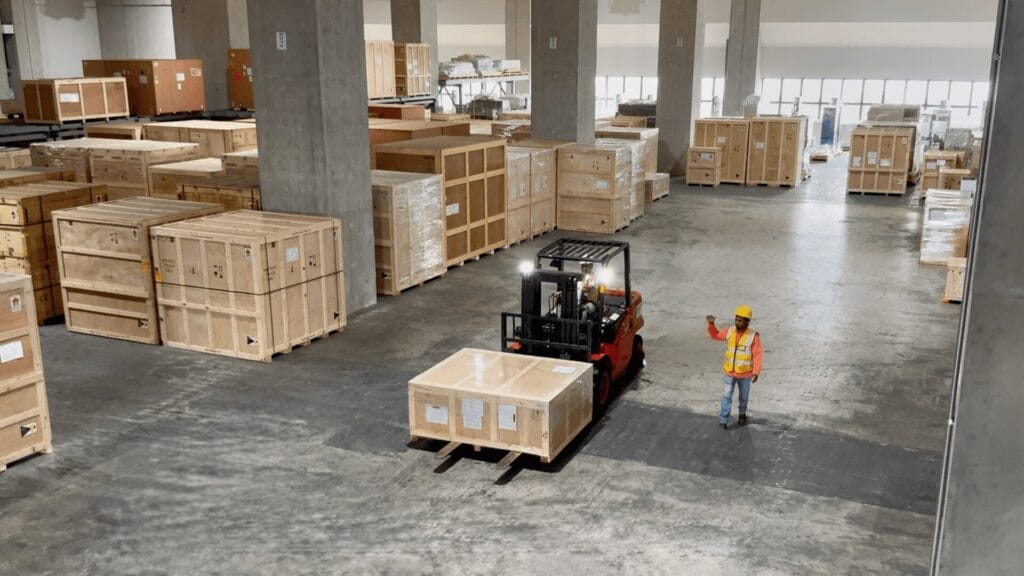
- Sustained handling standard across the full programme. The same cleanroom protocols, rigging discipline, and pedestal alignment procedures applied to the last tool as to the first. Programme scale did not dilute the standard.
- Controlled custody from warehouse to cleanroom floor. Every tool was received, stored, and released in the sequence the fab required — regardless of the order it arrived.
- No contamination events in completed cleanroom zones. Despite active construction running alongside the move-in throughout the programme, the cleanroom protocols established at the start held for the duration.
Why B H S Stands Out
High-volume programme execution is a different discipline from single-project work. At this scale, the planning, the warehouse staging, the sequencing, the site coordination, and the team management all have to function together — and they have to function consistently over weeks, not hours.
B H S has the operational capacity to run a programme of this kind without degradation. The warehouse is large enough to stage tools arriving from multiple countries simultaneously. The fleet is large enough to move tools to site in the sequence required without creating bottlenecks. The team is experienced enough to maintain cleanroom and rigging discipline throughout a physically demanding, extended programme.
At more than 100 tools, the margin for error is small. The consequences of losing control of the sequence, or of a handling standard that varies across the programme, reach the go-live date and the customer’s public commitment. B H S understands what is at stake and plans accordingly.
Broader Applications
- Fabrication facilities opening new fabs or expanding production capacity commission B H S for move-in programmes that span weeks, involve multiple tool types and pedestal specifications, and run alongside active construction.
- Semiconductor equipment manufacturers and OEMs supporting large-scale customer installations commission B H S as the programme execution partner at the receiving fab.
- Engineering, procurement, and construction firms delivering new fab build-outs commission B H S as the specialist rigging subcontractor for the tool and pedestal scope.
- Freight forwarders managing large tool shipment programmes commission B H S for the in-country physical handling scope — airside collection, warehouse staging, sequenced transport to site, and cleanroom rigging — as a single coordinated operation.
Conclusion
A complete semiconductor tool move-in is not a logistics exercise. It is a precision programme that runs on sequencing, discipline, and sustained operational performance against a deadline that cannot move.
B H S managed a programme of more than 100 tools and bespoke pedestals, sustained across weeks of execution, on a site where construction and cleanroom work ran side by side. The go-live date was met. The handling standard held.
For semiconductor manufacturers, OEMs, EPCs, and freight forwarders managing large-scale tool move-in programmes, B H S provides the capacity, the capability, and the programme discipline the work demands.
Contact us to discuss how B H S can support your next complete tool move-in programme.


